
Fabric Waviness: From Root Cause to Controlled Recovery
Challenge
A monsoon-season delivery of 8,760 m of 95% cotton/5% elastane single jersey arrived in 42 rolls; after unwinding and relaxation, 28 rolls covering 5,840 m showed edge and centre waviness. Under the normal 180 cm marker, matching leg panels differed by 8-22 mm along critical inseams and side seams and could not be stitched consistently without forced stretching, excessive easing or unauthorised trimming.
Action
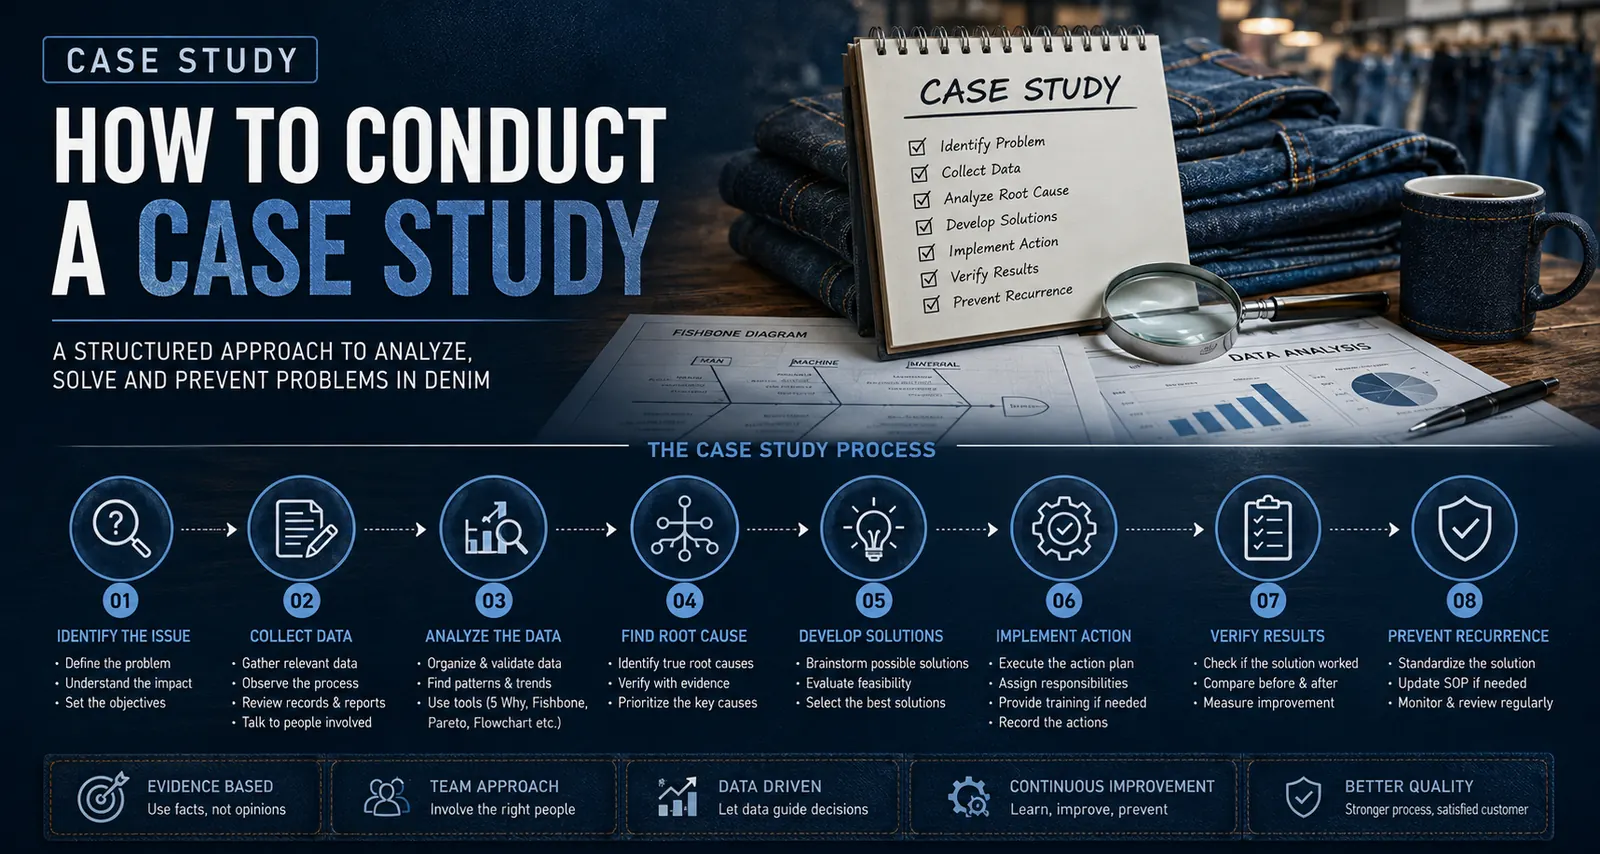
Every implicated roll, cut bundle and traceable garment was held and mapped, then affected and conforming material was compared under equivalent conditions from yarn through finished garment. Investigation confirmed cross-width overfeed imbalance during compacting created unequal residual length while excessive, inconsistent winding tension restrained it inside the roll; monsoon humidity activated the stored strain, and a 12-hour factory relaxation practice amplified panel variation without generating the original instability. A narrow 168 cm marker route was validated through panel and finished-garment trials with the supplier involved.
The supplier owned the manufacturing correction and the factory owned its relaxation and release control. Of the affected material, 4,960 m was released on the 168 cm narrow marker, 420 m after removing mapped sections, 260 m was rejected and replaced, and 200 m was consumed by trials and controlled cutting loss - recovering 5,380 m in total. Pilot and bulk garments met dimensional and appearance requirements, and three subsequent lots totalling 25,460 m showed no recurrence.
A monsoon-season delivery of 8,760 m of 95% cotton/5% elastane single jersey arrived in 42 rolls; after unwinding and relaxation, 28 rolls covering 5,840 m showed edge and centre waviness. Under the normal 180 cm marker, matching leg panels differed by 8-22 mm along critical inseams and side seams and could not be stitched consistently without forced stretching, excessive easing or unauthorised trimming.
Every implicated roll, cut bundle and traceable garment was held and mapped, then affected and conforming material was compared under equivalent conditions from yarn through finished garment. Investigation confirmed cross-width overfeed imbalance during compacting created unequal residual length while excessive, inconsistent winding tension restrained it inside the roll; monsoon humidity activated the stored strain, and a 12-hour factory relaxation practice amplified panel variation without generating the original instability. A narrow 168 cm marker route was validated through panel and finished-garment trials with the supplier involved.
The supplier owned the manufacturing correction and the factory owned its relaxation and release control. Of the affected material, 4,960 m was released on the 168 cm narrow marker, 420 m after removing mapped sections, 260 m was rejected and replaced, and 200 m was consumed by trials and controlled cutting loss - recovering 5,380 m in total. Pilot and bulk garments met dimensional and appearance requirements, and three subsequent lots totalling 25,460 m showed no recurrence.